A sourcing specialist I chat with sometimes called us up in a bit of a panic this week, and his question captures somethin' we hear from time to time. He had two quotes on the same custom 4" Class 150 alloy steel slip-on flanges for a routine cooling water line, but he didn’t know which one to go with. Supplier A came in at $850 each with Positive Material Identification (PMI) certificates included. Supplier B was $620 without PMI and told him to go get it done somewhere else. Well, dat price difference was a mighty noticeable percentage. He wanted to know if PMI was worth it for that job, or if he was payin' for paperwork he didn't actually need. What's a fella to do?
I'll tell you what, the answer depends on what assembly dem flanges are goin' into, and so what they're meant for. We reckon Supplier A put PMI on the quote 'cause the drawing called for it in the notes section. Now, for routine carbon steel in non-critical service, PMI is usually overkill. But for alloy steel, sour service, or anything where a material swap could kill the joint, it's the cheapest insurance you can buy. Here's how we walk folks through the pros and cons, and finally the decidin'.
What PMI Actually Is and What It Don't Do
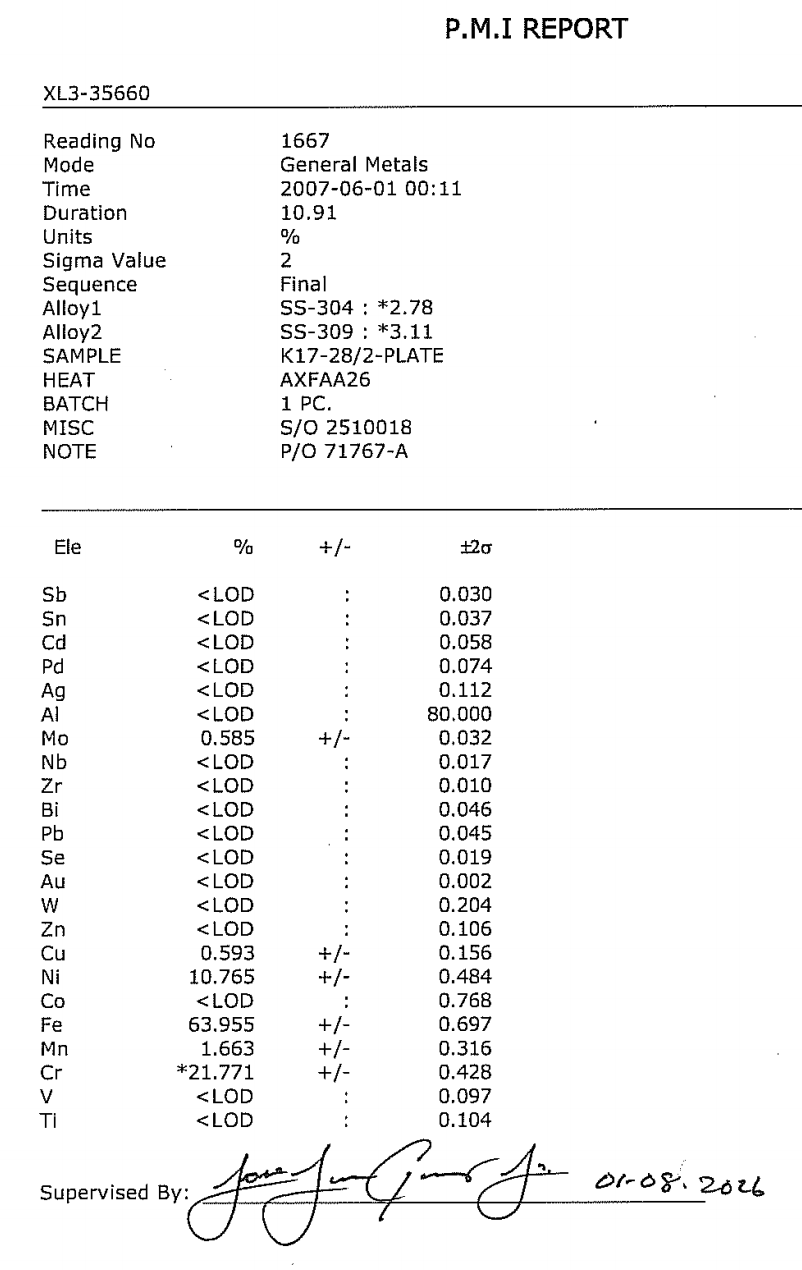
Positive Material Identification is non-destructive testin' that confirms what alloy a metal part is made of. The most common way on flanges is X-ray fluorescence (XRF) with a handheld analyzer. Folks call it a PMI gun or a “ray” gun, and it's a fun little piece of gear, like somethin' you'd have figured you'd only see on Star Trek. The technician points the gun at a clean spot on the flange OD, pulls the trigger, and in just a few moments he's got a readout of the alloy. What comes out is a certificate listin' the percentages of chromium, nickel, molybdenum, manganese, and other alloyin' elements it found.
What XRF does right well is tell alloy families apart. It'll cleanly tell you if a flange is A105 carbon steel, A182 F304 austenitic stainless, F316L higher-molybdenum stainless, F22 chrome-moly, Inconel 625, or Hastelloy C276. It does it by spottin' the elemental fingerprint of each alloy and the percentage makeup from there.
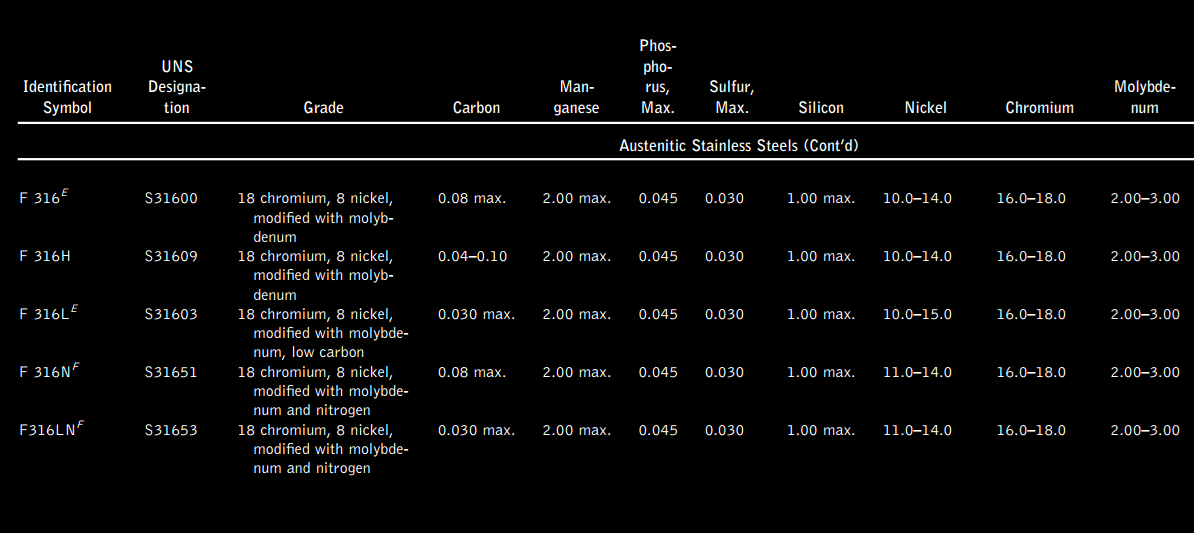
What XRF don't do is detect carbon directly. The energy carbon gives off when it gets hit with X-rays is too low for handheld units to pick up. That means XRF by itself can't tell 316 from 316L stainless (the L kind has lower carbon, which matters for corrosion resistance after weldin') or A105 from A350 LF2 (similar chemistry, different impact toughness requirements). To check them differences, y'all need either Optical Emission Spectroscopy (OES, which is handheld too but uses a different detection method that can read carbon) or wet chemistry from a lab.
The other thing XRF can't tell you is mechanical properties. The same chemistry can turn out different yield strength, tensile strength, and hardness dependin' on the heat treatment. A material that passes PMI as F22 might still be out of spec on hardness on account of bad heat treatment. PMI basically verifies what family the metal come from, but it don't verify how it got processed.
The American Society for Nondestructive Testing keeps the certification programs that govern how PMI gets done out in the field. Their PMI resource page is a mighty useful reference for understandin' what the technique can and can't do.
What the Mill Test Report Already Tells You
A Material Test Report (MTR) from the mill is available on request for the flanges we supply. The MTR documents:
Chemical composition from the heat (the batch of metal the flange was forged from)
Mechanical properties (yield, tensile, elongation, hardness) tested on coupons from the same heat
Heat treatment performed if applicable
Heat number, traceable back to the mill's records
Compliance with the applicable ASTM specification (A105, A182, A350, etc.)
If the MTR is from a reputable mill and the heat number on the flange matches the heat number on the MTR, well, you got documented proof of what the material is and how it performs. For most service, yessir, that's plenty.
PMI does somethin' different. It checks the flange in your hand against the documented chemistry. It catches three ways things go wrong that the MTR by itself usually don't:
Material substitution at the mill or distributor. Somebody swapped in a cheaper grade and forged up the paperwork, ain't that somethin'.
Mixin' durin' handlin'. A correct flange got separated from its MTR somewhere between the mill and your warehouse, and the MTR you're holdin' is for a different flange.
Counterfeit material. The flange never was made by the mill named on the certificate. In a clean supply chain with traceable mill sources, these problems are rare. But in a globalized, multi-tier supply chain with pressure to find cheaper sources, they ain't rare enough to ignore. That's one reason we talked in a recent post about sourcin' domestic whenever possible, to help handle this by dealin' direct with suppliers.
When the Premium Is Worth It
PMI earns its keep when the cost of a wrong material is high compared to the price of the testin'. Critical service applications often call for it. The clearest cases:
Sour service per NACE MR0175 / ISO 15156. If H2S is in the process fluid, the flange material has to be on the NACE-approved list AND meet hardness limits AND have proper heat treatment documentation. Say, for instance, a flange gets swapped from F316L to F316 (higher carbon, more prone to hydrogen-induced crackin') — you can't see that with your eyes and you can't catch it from the MTR review alone… well then, PMI catches it for you. The downside of gettin' this wrong and lettin' it go in is a crack failure in service, which on a wellhead or process unit costs orders of magnitude more than the PMI fee.
High-nickel alloys (Inconel 625, Hastelloy C276, Monel 400, Alloy 825). These materials cost eight to fifteen times more per pound than carbon steel. The money reason to substitute is enormous, and counterfeitin' in this category is rare but a documented problem in the industry. If y'all are buyin' high-nickel flanges, PMI on every part is standard practice for most experienced specifiers. You absolutely gotta confirm the material in field use to dodge replacement costs. The risks are just too hard on the budget otherwise.
Critical pressure boundaries. Anything where a leak or rupture would cause a safety incident, environmental exposure, or a major production loss. Pressure vessel nozzles, primary loop pipin' in power generation, high-pressure hydrogen service, anything carryin' lethal fluid per ASME B31.3 Category M. The PMI cost is a rounding error against what could happen, given the liability to life and property. Safety comes first, I tell you what!
Cryogenic and low-temperature service. A350 LF2 and LF3 have specific impact toughness requirements that come from controlled chemistry and heat treatment. A carbon steel substitute that meets A105 chemistry will still fail at LNG temperatures 'cause the impact properties are different. PMI plus the MTR review catches dat.
Government-funded infrastructure with Buy American or BABA requirements. Domestic-origin verification often pairs up with PMI as part of the documentation package. If you're subject to an AIS audit, PMI gives you part of the evidence chain.
When you don't know the supply chain. If you're buyin' from a new distributor, a broker, or a source you can't trace back to a known mill, PMI is the verification step that protects you. Again, sourcin' domestic helps right there.
When the Premium Is Not Worth It
That cooling water example at the top of this article is a case where we wouldn't push the customer toward PMI. Here's why:
Routine carbon steel in a benign service. A105 in fresh water at 110°F is forgivin'. A material swap within the carbon steel family (A105 to A350 LF2, for example) wouldn't cause a service problem.
Low consequence of failure. A leak on a cooling water line is an inconvenience, not a safety incident. The leak gets caught at hydrotest or first commissionin'. A material swap don't cause a catastrophic failure in this duty.
Known supplier with traceable mill source. If you've been buyin' A105 from the same supplier for a decade and they got a documented chain back to the mill, you ain't in the failure territory that PMI protects against.
Low value per flange. When the flange itself costs $200, payin' $150 for PMI is a big percent bump for a benefit you don't need. The risk-adjusted cost just don't pencil out.
For this kind of routine procurement, the MTR with verified heat number traceability is enough. MTRs are available on request at no extra charge.
The Middle Ground
A whole lot of buyin' decisions sit between "obvious yes" and "obvious no." Three ways we recommend for the middle:
PMI by sample, not by part. For a big order of routine flanges, test 10 to 20 percent of the lot. If the sample matches the MTR, take the rest. If the sample fails, step it up to 100 percent. That gets you most of the protection at a fraction of the cost.
PMI on first-article only. For a new supplier or a new material grade, PMI the first shipment. Build the supplier relationship on verified data. Once you got some history, drop down to MTR review only.
PMI on critical service only within a mixed order. If you're orderin' thirty flanges and four of 'em are goin' into critical service, PMI them four and take the MTRs on the rest.
These ways let you put your testin' money where it actually cuts risk, 'stead of spreadin' it thin across parts that don't need it.
What to Ask Your Supplier
Before you pay for PMI, make sure you know what's actually included.
Who performs the test? Is it done in-house at the supplier, or by third-party inspection? Third-party is more rigorous but adds cost and time. In-house is faster and cheaper if the supplier's got a calibrated XRF and a trained operator, but third party is more reliable since you control the process. It’s generally best to contract it yourself once you receive the material.
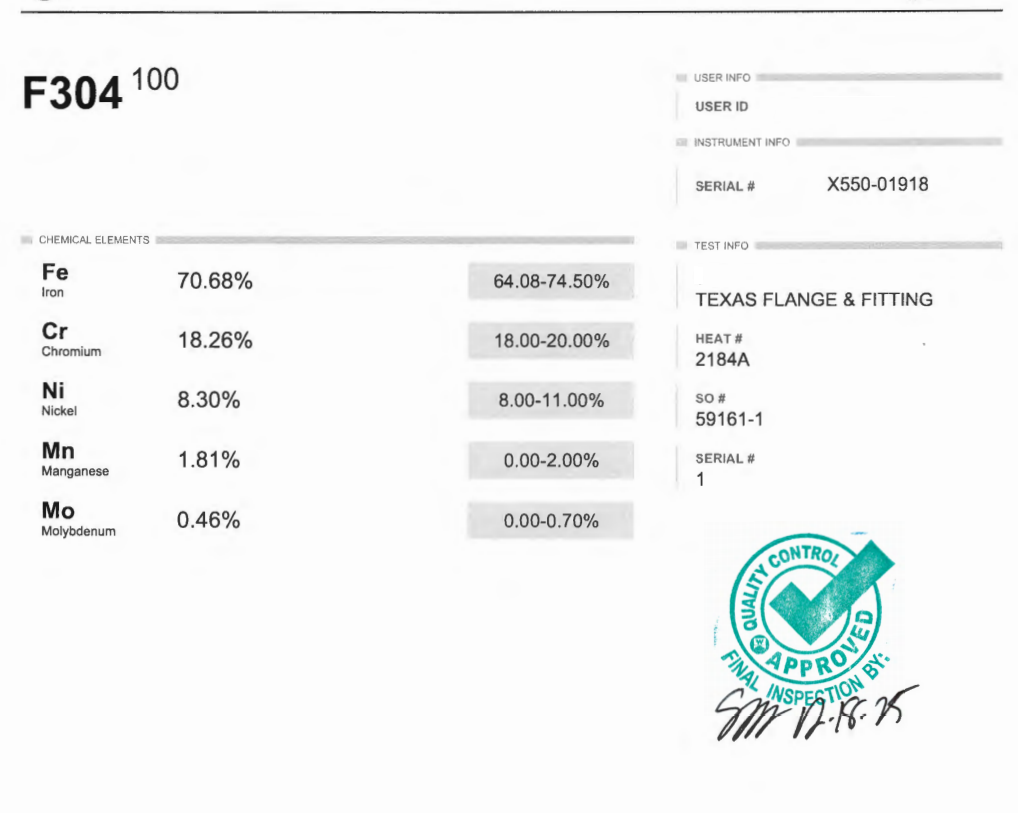
What is documented? A PMI certificate ought to list the analyzer model, calibration date, technician's name and certification level, the specific alloy detected, and the percentage breakdown of the elements found. A piece of paper that just says "PMI passed" ain't adequate documentation, no sir.
Is the test against the MTR or against the alloy spec? PMI against the MTR confirms the flange matches the paperwork. PMI against the alloy spec confirms it meets ASTM requirements. For most jobs you want both, since the MTR should already conform to the spec.
How is the test point selected? XRF measures a little spot on the surface. Surface contamination, paint, or an oxide layer can throw off the reading. The test point ought to be ground or wire-brushed down to clean metal.
A supplier who can answer these questions plain and hand over a sample PMI certificate is treatin' the test like a real quality step. A supplier who hems and haws could be sellin' you a piece of paper without much behind it.
The Bottom Line
PMI ain't a universal requirement. It's a risk management tool that pays for itself when the cost of a wrong material is high or when the supply chain's got gaps. For routine carbon steel in benign service from a known supplier, the MTR is enough. For high-nickel alloys, sour service, critical pressure boundaries, and cryogenic work, PMI is cheap insurance.
The question to ask ain't "should I always pay for PMI?" The question is "what's it cost me to be wrong about this material, and what's it cost to verify I'm right?" When the first number is big and the second is small, PMI is worth it, oh yeah.
If y'all are workin' through a flange specification and want help decidin' where PMI fits in your quality plan, send us the specs and the service conditions and we'll walk through it with you. For background on the paperwork that comes with a Texas Flange order whether or not PMI gets added, our guide on verifying flange material grades covers what the MTR documents and how to read it.
Texas Flange & Fitting Supply | 281-484-8325 | texasflange.com