Hydrogen ain't nothin' new to industry, no sir. Refineries been runnin' on it for decades for hydrocrackin' and desulfurization, and ammonia plants been handlin' it by the boatload since long before anybody said "energy transition." What's new is where it's headed: pipeline blendin', fuelin' infrastructure, and dedicated hydrogen production. That means "hydrogen service" is showin' up on specs in front of buyers who never had to think about it before, and hydrogen don't act like the natural gas or process fluids dey're used to.
Two things make hydrogen a problem for a flanged joint. It attacks de steel, and it leaks. A flange dat's perfectly sound on a crude line can be de weak link on a hydrogen line. Here's what "hydrogen-ready" really means once you get past all de marketin', y'all.
The Two Problems Hydrogen Creates
De first problem is hydrogen embrittlement. Hydrogen is de smallest atom dere is, small enough to work its way into de crystal structure of steel. Once it's in dere, it cuts down de steel's ductility and toughness, and under steady stress dat can lead to crackin' de material never would've seen otherwise. De risk ain't de same across all steels. It gets worse as strength and hardness go up, which is exactly backwards from how engineers usually think about pickin' a "stronger" material. In hydrogen, harder and stronger can mean more brittle, I tell you what.
De second problem is leakage. Dat same tiny molecule dat slips into de steel also slips through any path a seal leaves open. A gasket and surface finish dat hold a 600# steam joint without a weep can still pass hydrogen. Sealin' hydrogen is a tighter game than sealin' almost anything else, and it's gotta stay tight through thermal and pressure cyclin', not just on de day of de hydro test.
What ASME B31.12 Wants From the Material
Hydrogen piping in de U.S. is governed by ASME B31.12, de Hydrogen Piping and Pipelines code. It's dere for just dis reason: de general piping codes don't fully cover embrittlement. For flanges, two things drive de material selection, y’all.
First off, austenitic stainless steel is de baseline. Type 316 and especially 316L are de most stable austenitic grades and hold up pretty well against hydrogen embrittlement even in high-pressure gaseous hydrogen, 'cause de austenitic structure don't embrittle de way higher-strength ferritic and martensitic steels do. For a lot of hydrogen flange applications, solution-annealed 316L forgings are de safe default, and de solution anneal also relieves residual stress.
Second, B31.12 puts hard limits on de things dat drive embrittlement: carbon equivalent and hardness. De code generally caps hardness around 22 HRC for de materials it allows in hydrogen service. Carbon steel like A105 can be used in some gaseous hydrogen applications within de code's pressure, strength, and hardness limits, but dat hardness ceiling is doin' real work, and it ain't optional.
If dat 22 HRC number sounds familiar, it should. De same ceiling shows up in NACE MR0175 for sour service. But don't go reckonin' de two are interchangeable. Sour service guards against sulfide stress crackin' caused by H2S; hydrogen service guards against embrittlement from hydrogen itself. Dey land on similar hardness limits by different roads, and a flange qualified for one ain't automatically qualified for de other. If your service has both, it's gotta satisfy both. Our guide to NACE MR0175 sour-service flanges covers dat side in detail.
Sealing It So It Stays In
Material gets you a flange dat won't crack. Sealin' gets you one dat won't leak, and with hydrogen dat's its own discipline, y'all.
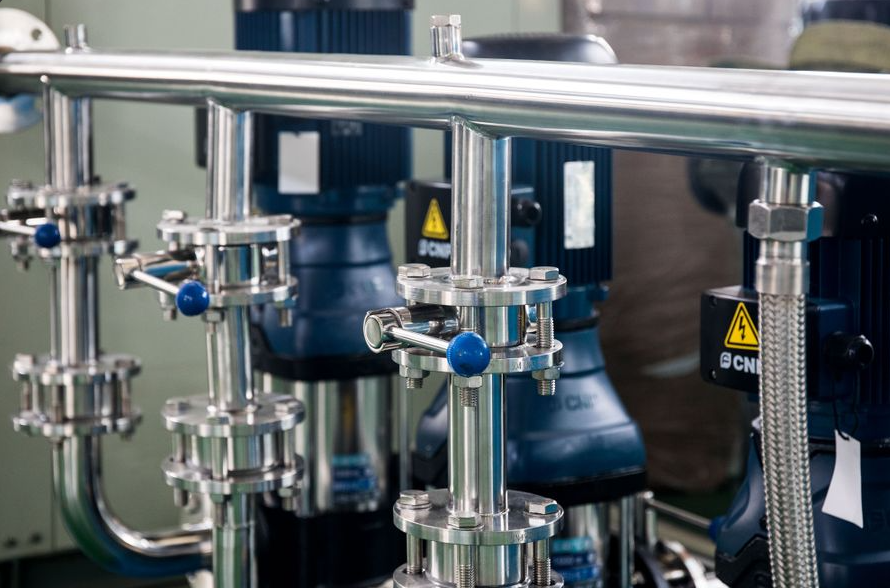
Weld neck flanges are preferred for de integrity of de joint and de smooth bore. Threaded connections are generally avoided in hydrogen service 'cause every thread is a potential leak path. As pressure climbs, de ring type joint (RTJ) becomes de connection of choice, 'cause a metal-to-metal seal seated in a machined groove holds hydrogen a whole lot better than a flat gasket squeezed between raised faces. For lower-pressure service, gasket selection still matters more than usual: de seal's gotta keep its stress through cyclin' and ideally come with real leakage qualification data behind it, not just some generic rating. Our RTJ flange guide walks through where de metal seal earns its keep.
One detail dat gets overlooked: de boltin'. Hydrogen embrittles high-strength fasteners too, and boltin' is often de highest-hardness steel in de whole joint. De bolt spec has to respect de same embrittlement limits as de flange, or de joint's weakest link becomes de studs holdin' it together.
A Hydrogen-Service Flange Checklist
Concern | What It Means | Spec Response |
Embrittlement | Hydrogen reduces steel ductility, worse at high hardness | 316/316L baseline; hardness capped ~22 HRC per B31.12 |
Governing code | General piping codes do not fully cover hydrogen | Specify to ASME B31.12 |
Residual stress | Raises cracking susceptibility | Solution-annealed 316L forgings |
Leakage | Smallest molecule finds any path | Weld neck, RTJ at higher pressure, qualified gaskets |
Bolting | Fasteners are often the hardest steel present | Bolt material held to the same hardness limits |
Sour + hydrogen | Different cracking mechanisms, similar limits | Must satisfy both NACE MR0175 and B31.12 |
The Bottom Line
"Hydrogen-ready" ain't a sticker, it's a set of decisions: a material dat resists embrittlement, a hardness held under de code limit, a seal built to keep de smallest molecule dere is from findin' daylight, and boltin' dat follows de same rules as de flange. Get dem right and de joint is as reliable as any in de plant. Treat a hydrogen line like a natural gas line and you're designin' in de failure, I reckon.
If you got a hydrogen project, whether it's a blendin' pilot, a production unit, or a fuelin' skid, and you want de flanges specified to ASME B31.12 with de right material and documentation, send us de line conditions. We'll get you hydrogen-compatible flanges, in 316L or code-compliant carbon steel, with de certs to prove it, right quick.
Texas Flange & Fitting Supply | 281-484-8325 | texasflange.com